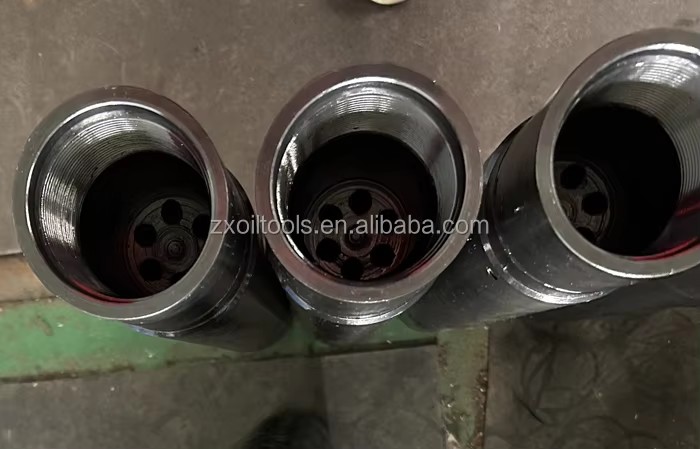
Oilfield Multistage Downhole Gas Separator for PC Pump Use in Well Drilling
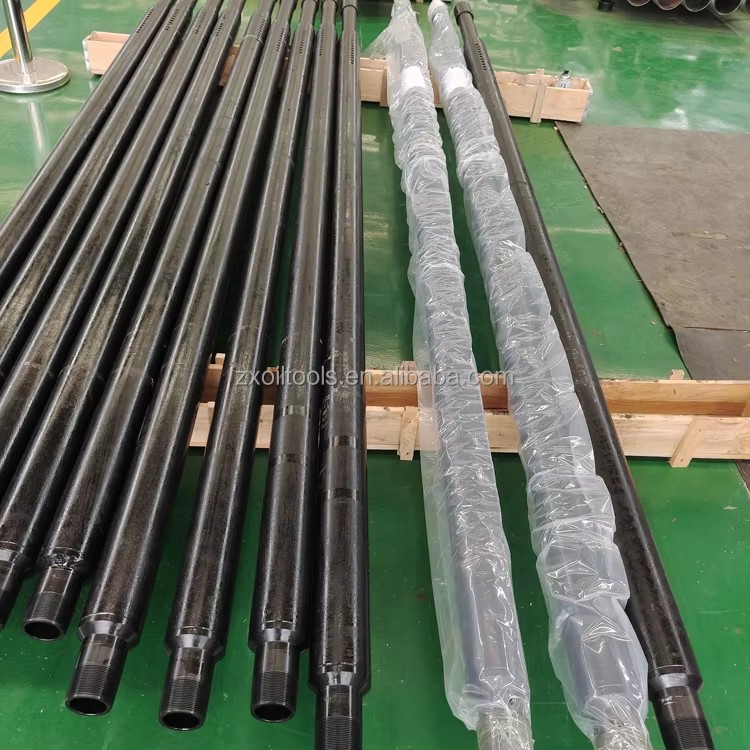
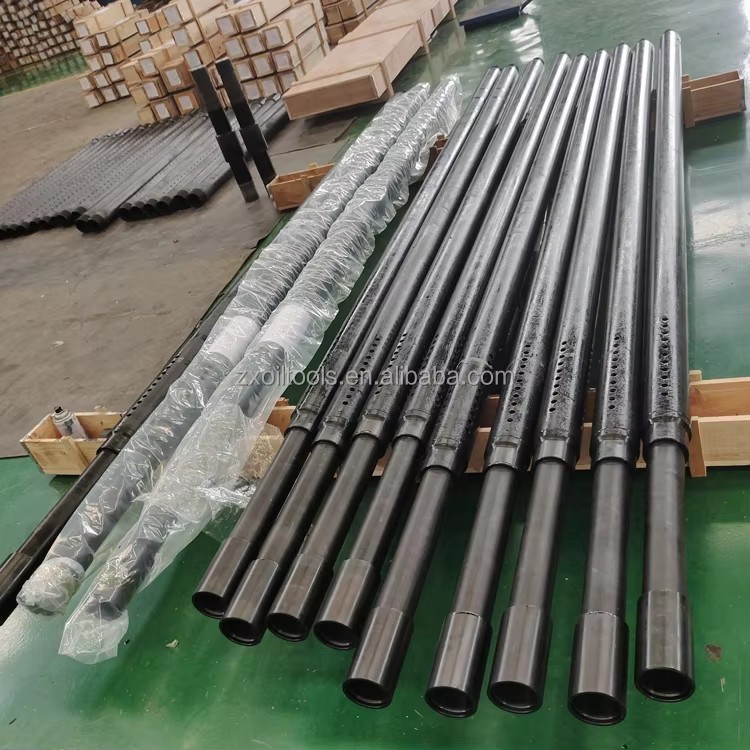
The Gas Anchor, downhole gas Separator has been designed as a continuous flow downhole gas separator to be used in conjunction with progressing cavity pumps.
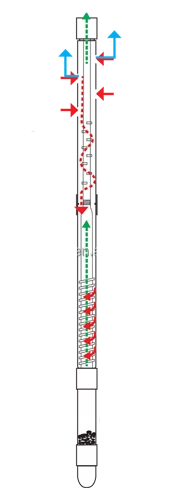
The downhole gas Separator was designed to provide a method of allowing gas to separate out of the solution and migrate up the annulus, preventing gas locking of the down-hole pump.
Working principle
The gas Separator use centrifugal forces to separate the gas from the produced liquids, before they enter the pump. Liquids will be carried through into the pump suction while the separated gases are forced to migrate up the annulus.
Advantages: 1)The pump efficiency and pump rate will be increased. 2) Elimination CO2 and H2S before they enter the pump will extend it’s life.
| Type | LZX-113 | LZX-140 |
| Max OD mm | 113 | 140 |
| Max OD of cup mm | 132 | 165 |
| Connection thread type | 2 7 / 8 TBG | 2 7 / 8 TBG |
| Max length mm | 3200 | 3200 |
| Suitable casing size in | 5 1 / 2 ’’ | 7 ’’ |
A: Your inquiry related to our products or prices will be replied in 24 hours. B: Protection of your sales area, ideas of design and all your private information. C: Best quality and competitive price.


-
Step 1
Payment and order readiness
Minimum order: 5 Units
Payment terms, specifications, and order details are confirmed before preparation begins.
-
Step 2
Preparation
25 days
-
Step 3
Packaging and dispatch
Packaging details are available on request.
Final packing, freight, and delivery dates are confirmed before dispatch.
Customer reviews
No reviews yet
Be the first customer to review this product.
Write a review
Request custom sourcing
Can’t find what you’re looking for? Share the requirement and our sourcing team will find the right industrial product.